+86 13163919000
 info@xinmeiintelligent.com
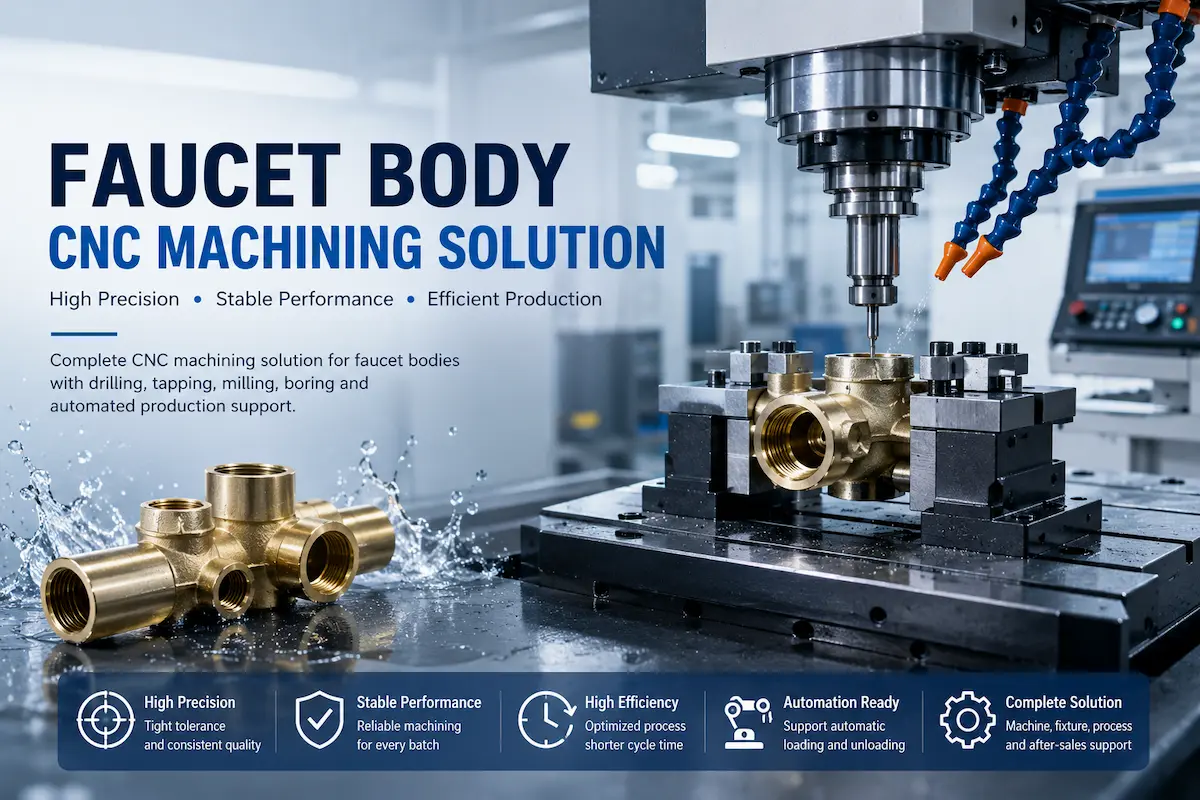
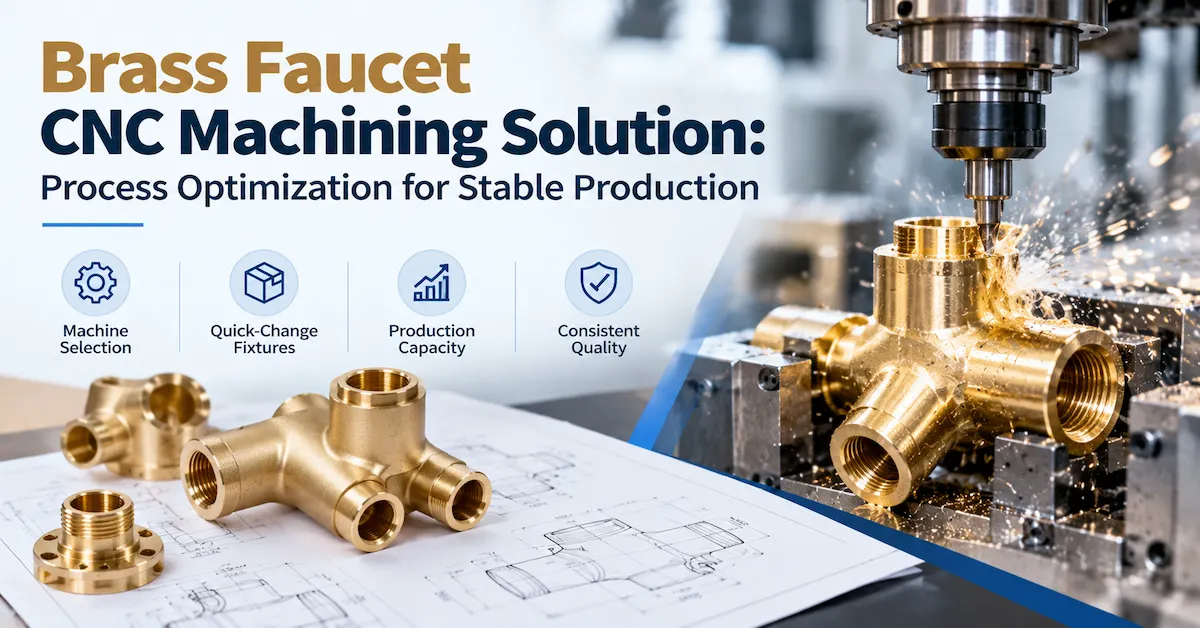
A brass faucet CNC machining solution for mixed-model production must balance machining accuracy, equipment flexibility, changeover time, and accepted production output. For faucet manufacturers producing several body designs, the most expensive mistake is selecting a machine that performs well on one component but becomes inefficient whenever the production schedule changes.
The right solution combines suitable CNC equipment, repeatable workholding, controlled machining programs, quality verification, and a realistic production-capacity plan. Multi-spindle equipment may suit repeated part families, while flexible machining centers can be more practical when dimensions, port positions, or batch quantities change frequently.
This guide helps sanitary ware manufacturers, production engineers, and equipment buyers evaluate CNC machine configurations, reduce changeover risks, and prepare a technically meaningful purchasing specification.
Explore XINMEI Bathroom Hardware Machining Solutions | Request a Customized CNC Solution
1. What Is a Brass Faucet CNC Machining Solution for Mixed-Model Production?
A brass faucet CNC machining solution is an integrated manufacturing approach covering machine selection, fixtures, tooling, machining programs, inspection, and production workflow. In mixed-model manufacturing, it must also accommodate multiple component designs without excessive equipment adjustments or lengthy setup interruptions.
A faucet manufacturer may produce concealed faucet bodies, mixer housings, valve components, and threaded connection parts on the same production floor. Although these components share machining processes, their geometry, locating features, tool access, and critical dimensions may differ.
A practical solution should answer five questions:
-
Which faucet components can share the same CNC equipment?
-
Which fixtures and tools can remain common between models?
-
How quickly can production switch between approved part designs?
-
Can the equipment meet the required quantity of accepted parts?
-
How will dimensional and functional quality be verified after each changeover?
The main objective is not the shortest possible machining cycle for one part. It is reliable production across the complete product mix.
This distinction matters when manufacturers supply several faucet designs, respond to changing orders, or produce OEM bathroom hardware for different customers.
2. Which Faucet Manufacturers Benefit Most From a Flexible CNC Solution?
Not every faucet factory needs the same machine configuration.
The appropriate production system depends on product variety, batch volume, order stability, and the relationship between component designs.
| Manufacturing situation | Main challenge | Recommended direction |
|---|---|---|
| Several faucet body models produced weekly | Frequent fixture and program changes | Flexible CNC machining center |
| Similar brass bodies with repeated hole patterns | High machining demand across related components | Multi-spindle CNC configuration |
| One standardized faucet body produced continuously | High-volume output and repeatability | Special-purpose CNC equipment |
| Multiple models requiring several machining directions | Repeated repositioning and complex tool access | Multi-axis or horizontal machining solution |
| Stable component families with repetitive manual handling | Loading consistency and labor availability | CNC automation evaluation |
When Is a Dedicated CNC Machine Less Suitable?
A dedicated machine may be less attractive when production volumes are uncertain, part geometry changes frequently, or future products require significantly different machining operations.
Highly specialized fixtures and fixed spindle arrangements can become costly to modify.
Conversely, a general-purpose machining center may be unnecessarily flexible when one standardized component accounts for most production demand.
Buyers should compare equipment against their projected product mix rather than selecting based on spindle count or advertised machining speed alone.
3. Build a Faucet Part-Family Matrix Before Selecting Equipment
A part-family matrix groups components according to the machining features and equipment requirements they share.
This is an important early step because two faucet bodies may look similar while requiring different clamping positions, cutting tools, or machining directions.
For example, a factory producing concealed faucet bodies and angle-valve housings should not automatically assume both components can use the same fixture.
What Information Should Be Compared?
| Evaluation item | What to record | Why it matters |
|---|---|---|
| Workpiece material | Exact brass alloy and blank condition | Influences tooling and machining parameters |
| Overall geometry | Dimensions, shape, locating surfaces | Determines machine travel and fixture design |
| Critical features | Bores, threads, ports, sealing interfaces | Determines machining and inspection requirements |
| Machining directions | Required spindle approach directions | Affects machine architecture |
| Common tools | Shared drill, tap, boring, and milling tools | Reduces unnecessary tool changes |
| Product variation | Features that change between models | Determines fixture and program flexibility |
| Batch requirements | Quantity per order and changeover frequency | Influences machine utilization |
| Quality criteria | Critical tolerances and acceptance methods | Supports consistent production approval |
Separate Common Features From Variable Features
If several faucet bodies share a common locating surface and connection geometry, engineers may be able to retain a fixture base while changing replaceable locating elements.
However, when casting shapes, datum relationships, or critical features differ substantially, separate fixtures may be more reliable.
The goal is to identify genuine component compatibility rather than forcing unrelated parts into a common fixture.
Buyer recommendation: Provide drawings for at least two representative faucet models, including the most complex and the most frequently produced component, before requesting a machine recommendation.
4. Which CNC Machine Configuration Is Best for Brass Faucet Production?
A well-designed brass faucet CNC machining solution should match machine architecture to the required operations and expected production mix.
XINMEI provides CNC machining centers, special-purpose machines, and industrial automation solutions for different manufacturing requirements.
CNC Machine Comparison for Faucet Manufacturers
| CNC equipment type | Main advantage | Best application | Main trade-off |
|---|---|---|---|
| Vertical CNC drilling and tapping machine | Efficient access for drilling and tapping | Faucet components with accessible holes and threads | Complex multi-face work may require repositioning |
| Flexible CNC machining center | Supports multiple tools and changing programs | Mixed-model faucet manufacturing | May have longer cycles than a dedicated system |
| Multi-spindle CNC machine | Can improve repeated machining efficiency | Similar parts with compatible operations | Requires careful spindle and fixture planning |
| Horizontal machining center | Useful for multi-directional machining | Complex valve and faucet housings | Greater investment and application-specific setup |
| Special-purpose CNC machine | Process-specific configuration | Stable, high-volume part families | Lower flexibility for unrelated products |
| CNC robotic production cell | Reduces repetitive manual loading | Stable part orientation and repeated production | Integration and changeover complexity |
Why More Spindles Do Not Always Mean More Output
A multi-spindle machine is valuable when its spindle arrangement matches the actual machining operations.
If the workpiece requires incompatible tool directions, repeated repositioning, or extensive changeovers, additional spindles may provide limited benefit.
Similarly, fast spindle movement does not eliminate loading time, tool changes, fixture adjustments, or quality inspection.
The correct comparison is between complete production cycles, not isolated spindle specifications.
For relatively accessible brass faucet components, XINMEI's Vertical CNC Drilling and Tapping Machine is one equipment category worth evaluating.
Final suitability depends on the actual part drawing, tooling arrangement, machining requirements, and production target.
5. How Can Quick-Change Fixtures Improve Faucet CNC Production?
Fixture changeover is often a major source of production interruption in mixed-model machining.
A CNC machine may switch programs quickly, but the complete changeover can still require fixture removal, cleaning, alignment, tool adjustment, work-offset verification, and first-piece inspection.
Design Fixtures Around Repeatable Location
A suitable fixture system should provide:
-
Reliable workpiece positioning against defined locating features.
-
Sufficient rigidity without damaging brass or finished surfaces.
-
Access to the required machining directions.
-
Effective chip clearance around locating surfaces.
-
Controlled replacement of interchangeable fixture components.
-
Repeatable loading and appropriate error-proofing.
For related faucet bodies, modular nests, replaceable locating elements, and compatible fixture bases may help simplify changeovers.
However, modularity should not weaken positioning or clamping stability.
XINMEI's technical resource on CNC Fixtures and Workholding explains why proper fixture design is essential to machining consistency.
Measure the Complete Changeover
For production planning, define changeover time as the period from the last accepted part of the previous model to the first accepted part of the next model.
This definition captures both mechanical setup and production approval.
| Changeover activity | Improvement opportunity |
|---|---|
| Fixture preparation | Prepare the next fixture before machine stoppage |
| Tool preparation | Preset compatible tools where practical |
| Workpiece loading | Standardize locating and clamping instructions |
| Program selection | Use controlled, revision-specific programs |
| Offset verification | Confirm approved offsets for each part family |
| First-piece inspection | Prepare gauges and inspection instructions in advance |
A shorter setup is only an improvement when the next component meets its required specifications.
6. Control Brass Machining Quality Across Different Product Models
Brass generally offers favorable machining characteristics, but different brass alloys and blank conditions can require different cutting strategies.
The selected material grade, casting or forging condition, wall thickness, and component geometry influence tooling and machining behavior.
For mixed-model faucet production, three areas deserve particular attention.
Thread and Bore Consistency
Faucet components may contain threaded ports, cartridge bores, and precision connection features.
The required thread form and tolerance must come from the approved drawing. Thread standards and gauges should not be assumed interchangeable between product markets.
After changing models, verify the correct tool, work offset, machining program, and inspection method before releasing the next batch.
Burrs and Internal Passage Cleanliness
Intersecting holes and internal channels can create burrs that affect assembly or downstream cleanliness requirements.
Deburring and chip removal should therefore be included in the defined process, not treated as optional finishing work.
The appropriate method depends on internal accessibility, component geometry, and the cleanliness criteria specified by the customer.
Protecting Sealing and Visible Surfaces
Faucet bodies may contain sealing-related faces and externally visible surfaces.
Fixture contact should avoid unacceptable marking or distortion. Inspection must also distinguish dimensional conformity from downstream functional leak testing, where required.
For further technical guidance, review XINMEI's article on CNC Machining Repeatability.
7. How Do You Calculate Real Production Capacity for Mixed-Model Faucet Machining?
Production capacity should be calculated from the complete manufacturing schedule, including all planned component models.
A supplier's shortest demonstrated cycle does not necessarily represent the output achievable during a full shift.
Use a Product-Mix Capacity Model
A practical planning formula is:
Required production time = Σ (Quantity per model × Complete cycle time per model) + Changeover time + Planned inspection time
The complete cycle should include applicable loading, unloading, cutting, tool changes, indexing, and other non-overlapping operations.
Illustrative Capacity Calculation
Consider a factory planning two brass faucet models during one shift.
| Production parameter | Example |
|---|---|
| Available production time | 450 minutes |
| Model A quantity | 180 units |
| Model A complete cycle | 60 seconds |
| Model B quantity | 120 units |
| Model B complete cycle | 90 seconds |
| One model changeover | 25 minutes |
| Planned first-piece inspections | 20 minutes |
The calculated time is:
-
Model A: 180 × 60 seconds = 180 minutes.
-
Model B: 120 × 90 seconds = 180 minutes.
-
Changeover and inspection: 45 minutes.
-
Total planned requirement: 405 minutes.
This leaves 45 minutes before reaching the 450-minute available-time limit.
However, that remaining time must absorb unplanned stoppages, additional checks, quality losses, and other operating variation.
These figures are illustrative planning assumptions, not measured XINMEI machine performance.
For consistent reporting, ISO 22400-2:2014 provides established terminology for manufacturing operations performance indicators.
A production proposal should clearly identify the calculation method, timing boundaries, and operating assumptions.
Why Accepted Output Matters More Than Theoretical Capacity
If a machine produces components quickly but requires frequent rework or dimensional adjustments, its usable output can be significantly lower than its theoretical capacity.
Purchasers should distinguish:
Theoretical cycles → Completed components → Inspected components → Accepted components
The final purchasing decision should consider accepted production output under agreed operating conditions.
8. How Should Manufacturers Validate Changeover and Machining Performance?
An effective equipment acceptance plan should test more than one easy-to-machine reference component when the machine is intended for mixed-model production.
The test should reflect the actual product families, process conditions, and quality requirements.
Recommended Acceptance Checks
| Test item | Verification requirement |
|---|---|
| Machine configuration | Confirm spindle, control, travel, tooling, and fixture specifications |
| Reference model | Machine approved sample components |
| Second product model | Complete an actual model changeover |
| Changeover time | Measure from last accepted part to first accepted part |
| Critical dimensions | Inspect drawing-defined bores, holes, and sealing features |
| Thread quality | Use specified thread gauges and inspection methods |
| Surface condition | Check clamping damage and required finishes |
| Production stability | Monitor cycle variation and interruptions |
| Accepted output | Count conforming components during the agreed test |
| Documentation | Retain test records, programs, and approved configurations |
ISO 230-2:2014 provides methods for assessing the positioning accuracy and repeatability of numerically controlled machine-tool axes.
However, machine-axis accuracy is not a substitute for verifying actual faucet dimensions, tool performance, fixture repeatability, or functional requirements.
For a customized system, buyers and suppliers should agree on the factory acceptance test (FAT), sample quantities, test duration, and acceptance criteria before manufacturing is completed.
9. When Should a Brass Faucet Factory Add Robotic Automation?
Automation can support repeatable loading and improve material flow, but it should not be introduced solely because a factory operates multiple CNC machines.
For a mixed-model faucet factory, the central question is whether automation can handle the required product variations without creating new delays.
Check Automation Readiness
A suitable project should consider:
-
Consistency of incoming brass blanks.
-
Repeatable workpiece orientation.
-
Compatible fixtures and grippers.
-
Robot access to the machine.
-
Model-specific loading programs.
-
Safe recovery from loading or clamping errors.
-
Changeover frequency and operator involvement.
A robot that handles one faucet body reliably may require additional tooling or programming for another body with a different shape.
Therefore, automation should be evaluated using the full product family rather than a single demonstration part.
XINMEI offers Robot Loading and Unloading Lines and broader Industrial Automation Solutions for applicable CNC production requirements.
For manufacturers with uncertain production mixes, starting with a flexible machining cell and evaluating automation after the processes are stable may be a more manageable investment strategy.
10. What Determines the Cost of a Brass Faucet CNC Machining Solution?
The total investment depends on the selected machine structure, production requirements, and scope of integration.
A quotation for a standalone CNC machine is not directly comparable with a proposal covering multiple fixtures, custom tooling, automatic loading, and complete system commissioning.
Evaluate Total Cost of Ownership
| Cost category | What buyers should include |
|---|---|
| CNC equipment | Machine configuration and control system |
| Tooling | Drills, taps, boring tools, holders, replacement tools |
| Fixtures | Dedicated or modular workholding systems |
| Changeover resources | Presetting tools, fixture elements, training |
| Inspection | Gauges, measuring equipment, quality procedures |
| Automation | Robots, grippers, conveyors, safety integration |
| Maintenance | Consumables, spare parts, planned servicing |
| Operating costs | Energy, labor, downtime, tooling replacement |
| Quality losses | Rework, scrap, rejected components |
A low purchase price may be attractive initially, but frequent model changes or production interruptions can increase operating costs.
Conversely, a complex automated line may not be economically justified when annual production quantities are limited.
Buyers should request proposals based on the same product mix, manufacturing assumptions, and acceptance requirements.
11. How XINMEI Supports Brass Faucet CNC Equipment Selection
XINMEI Intelligent supplies CNC machine tools and industrial automation solutions for manufacturing applications including bathroom and sanitary hardware.
Its published Bathroom Hardware Machining Capabilities include drilling, tapping, milling, turning, multi-spindle machining, and automated production for copper and brass components.
For a mixed-model faucet project, the engineering evaluation can focus on:
-
Reviewing representative faucet body drawings and material requirements.
-
Identifying common machining operations across product families.
-
Comparing flexible CNC and special-purpose equipment configurations.
-
Evaluating fixture, tooling, and changeover requirements.
-
Estimating production capacity using the planned product mix.
-
Determining whether automation is technically and commercially appropriate.
-
Establishing project-specific testing and acceptance requirements.
The purpose is to identify a suitable manufacturing configuration rather than assuming that one standard machine can process every faucet design.
Specific machine capabilities, customization scope, achievable cycle times, delivery schedules, and acceptance commitments must be confirmed for the proposed project.
Planning a new faucet production cell or upgrading existing equipment?
Contact XINMEI for an Engineering Review
12. What Should Buyers Include in a CNC Equipment RFQ?
A detailed request for quotation (RFQ) helps suppliers recommend equipment using actual production requirements instead of general assumptions.
For mixed-model faucet production, the RFQ should describe the complete component family.
| RFQ requirement | Information to provide |
|---|---|
| Product models | Drawings and revisions for each representative SKU |
| Material | Brass alloy, blank type, and incoming condition |
| Production mix | Annual and monthly quantities by model |
| Batch size | Typical order quantity per setup |
| Machining features | Bores, threads, holes, and critical surfaces |
| Quality requirements | Tolerances, inspection and functional criteria |
| Changeover target | Required frequency and acceptable setup duration |
| Existing process | Current machine types and operating limitations |
| Production target | Required accepted output per shift |
| Automation scope | Manual, semi-automatic, or robotic loading |
| Factory constraints | Space, utilities, operator availability |
| Acceptance conditions | Sample testing, FAT, documentation requirements |
When possible, include actual component samples and records showing current defects or process limitations.
The supplier can then evaluate different machine configurations against the same set of requirements.
A useful proposal should identify its technical assumptions, exclusions, and elements requiring further validation.
Frequently Asked Questions
1. What is the best brass faucet CNC machining solution for a factory producing multiple models?
The best solution depends on component similarity, batch size, critical dimensions, and changeover frequency. A flexible CNC machining center may suit changing product designs, while dedicated or multi-spindle equipment may be more attractive for standardized, high-volume components.
2. Can one CNC machine process different brass faucet bodies?
Yes, if machine travel, tooling, spindle access, fixtures, and machining programs can accommodate the required parts. Compatibility must be evaluated using actual drawings rather than assuming all faucet bodies share the same machining requirements.
3. How can a factory reduce CNC changeover time?
Factories can prepare fixtures and tools in advance, standardize locating systems, control CNC programs and offsets, and organize first-piece inspection. The total improvement should be measured from the last accepted part of one model to the first accepted part of the next.
4. Is a multi-spindle CNC machine better than a conventional machining center?
Not necessarily. Multi-spindle equipment can be advantageous for compatible repeated operations, but flexible machining centers may be better when product designs or machining directions change frequently.
5. What features are important when machining brass faucet bodies?
Critical considerations include threaded connections, precision bores, sealing interfaces, intersecting passages, fixture contact, chip removal, and surface condition. Exact acceptance requirements should follow the approved component drawing.
6. How should buyers calculate CNC production capacity?
Calculate the complete cycle time for each model, multiply it by the planned quantity, and add changeover and inspection time. Allow for expected production losses, and evaluate accepted output rather than only theoretical machine cycles.
7. Can robotic loading support mixed-model faucet production?
It may be suitable when workpiece orientation, fixture location, gripper design, and loading programs can be controlled across the required product range. Model changes and recovery procedures should be included in the automation study.
8. How should a customized CNC machine be tested before delivery?
Agree on a factory acceptance test using representative workpieces, verified dimensions, controlled machining conditions, an actual model changeover, and a defined accepted-output target. Machine positioning checks alone do not prove the entire machining process.
9. What affects the price of CNC equipment for brass faucet manufacturing?
Major factors include machine architecture, spindle configuration, CNC control, tooling, fixtures, automation, inspection requirements, customization, and service scope. Total operating cost should be considered alongside the initial equipment price.
10. How can I request a customized brass faucet CNC machining solution from XINMEI?
Prepare your faucet drawings, material specifications, production quantities, critical tolerances, model variations, and automation requirements. Submit these details through the XINMEI Contact Us page to discuss a suitable equipment configuration and project-specific quotation.
Conclusion
Selecting the right brass faucet CNC machining solution requires more than comparing machine specifications or choosing the shortest advertised cycle time. For mixed-model faucet manufacturers, long-term productivity depends on suitable equipment architecture, repeatable fixtures, efficient changeovers, stable machining quality, and realistic capacity planning.
A flexible CNC machining center may provide the best balance for frequently changing products. Multi-spindle and special-purpose machines may deliver greater value when component families and production quantities justify dedicated configurations. Automation should be added when it supports the complete manufacturing workflow rather than creating additional changeover complexity.
Most importantly, equipment performance should be validated using representative faucet bodies, agreed inspection requirements, and measurable accepted output.
XINMEI Intelligent provides CNC machines, customized machining configurations, and industrial automation solutions for bathroom hardware manufacturing.
If your factory is planning mixed-model brass faucet production, expanding capacity, or upgrading existing CNC equipment, contact XINMEI with your component drawings and production requirements to discuss a suitable manufacturing solution.